 Skip to main content Skip to footer

We have seen it happen more times than we would like to admit. A batch of wire EDM parts passes inspection at the factory, gets loaded into a container, crosses the Pacific — and arrives with rust on the cut faces. The buyer is angry. The supplier is defensive. And no one can agree on who is responsible, because the contract said nothing specific about packaging.
Rust prevention and packaging requirements for wire EDM parts should be written into the purchase order as hard specifications: a maximum post-machining-to-packaging interval, nitrite-free VCI bag with heat seal, desiccant inside the sealed envelope, individual part wrapping for precision components, and a zero-rust acceptance standard referenced to a recognized visual comparator such as SSPC-VIS 1.
If your contract currently says only "parts shall be rust-free," that clause is effectively unenforceable. The sections below will show you how to close every gap — from the moment the part leaves the EDM tank to the moment it arrives at your dock.
What Anti-Rust Packaging Standards Should I Specify for Steel Wire EDM Parts Shipped by Sea?
Ocean freight 1 is a harsh environment for freshly machined steel. Three to four weeks inside a container means temperature swings, humidity cycles, and — in the worst cases — "container rain," where condensation drips from the ceiling onto inadequately sealed packages. Wire EDM parts are especially vulnerable because the machining process leaves bare, chemically active steel surfaces with no protective scale or oxide layer.
For steel wire EDM parts shipped by sea, specify nitrite-free and amine-free VCI (Vapor Corrosion Inhibitor) bags or wraps as the baseline packaging material. Bags must be heat-sealed, not folded. Include desiccant sachets inside each sealed package. Specify a minimum 24-month protection rating for the VCI film.
Why Wire EDM Parts Rust So Easily
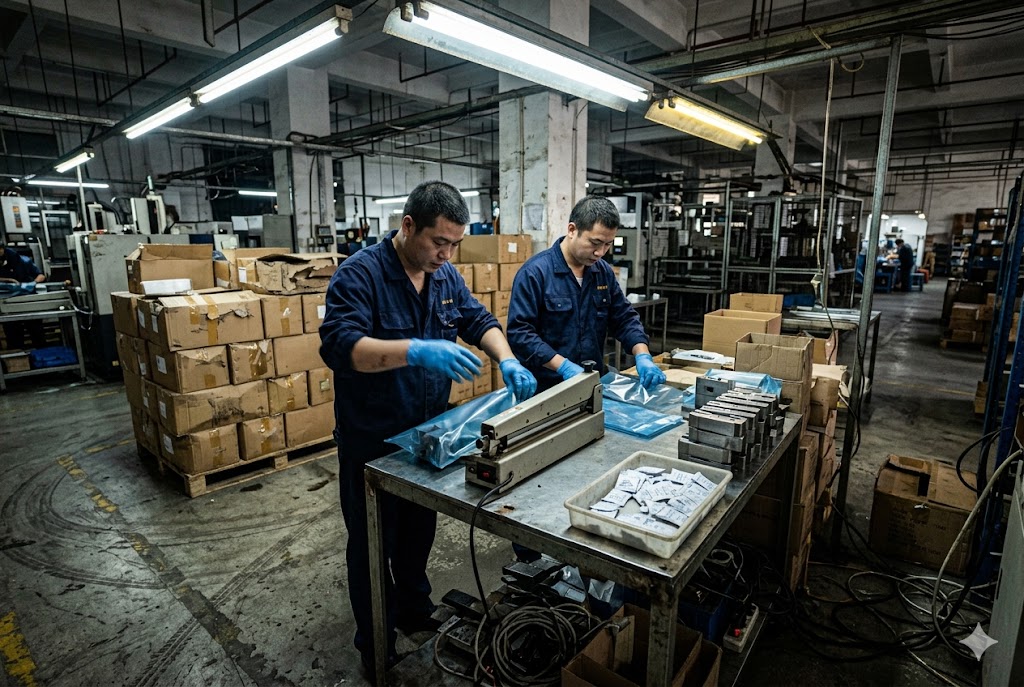
Wire EDM cuts steel by passing electrical current through deionized dielectric fluid 2. During cutting, steel ions dissolve into the dielectric fluid. Once the part is removed from the tank, the bare steel surface has no passive oxide layer 3 protecting it. The oxidation reaction starts almost immediately when the surface contacts humid air. This is different from a turned or milled part, where tool pressure and heat can leave a thin work-hardened layer on the surface.
The practical implication: you cannot treat wire EDM parts the same way you would treat standard machined parts when specifying packaging. They need a vapor-phase inhibitor 4 — not just a PE bag.
Specifying VCI Film: What to Name in the Contract
Do not write "VCI packaging required" and leave it there. Name the following parameters explicitly:
| Contract Parameter | Recommended Specification |
|---|---|
| VCI chemistry | Nitrite-free, amine-free formulation |
| Film format | Bag or wrap (state which) |
| Minimum film thickness | 100 microns (4 mil) for bags |
| Seal method | Heat seal only — folded closures are not acceptable |
| Protection duration rating | 24 months minimum (ocean freight standard) |
| Desiccant requirement | Silica gel or molecular sieve sachet inside sealed envelope |
| Substitution rule | Bare PE film or standard poly bags are not acceptable substitutes |
The substitution rule matters. Many Chinese factories stock standard polyethylene bags as their default. When the purchasing team is rushing a shipment, they will use whatever is on the shelf. If your contract does not explicitly prohibit substitutions, the supplier can argue that "packaging was used" and the claim is technically defensible.
The Container Rain Problem
Container rain 5 is condensation that forms inside a shipping container when warm, humid air entering the container at origin cools during transit. The moisture condenses on the container ceiling and drips onto cargo. Parts inside individual VCI bags that are only folded — not heat-sealed — are not protected against this. The fold opens slightly with moisture and pressure, and humid air enters the package.
Heat-sealing 6 is the only way to guarantee the VCI atmosphere inside the bag stays intact for the duration of ocean transit. This is not a premium specification. It is a baseline requirement for any precision ferrous part shipped across the Pacific.
How Do I Define Individual Part Wrapping, Desiccant, and VCI Bag Requirements Contractually?
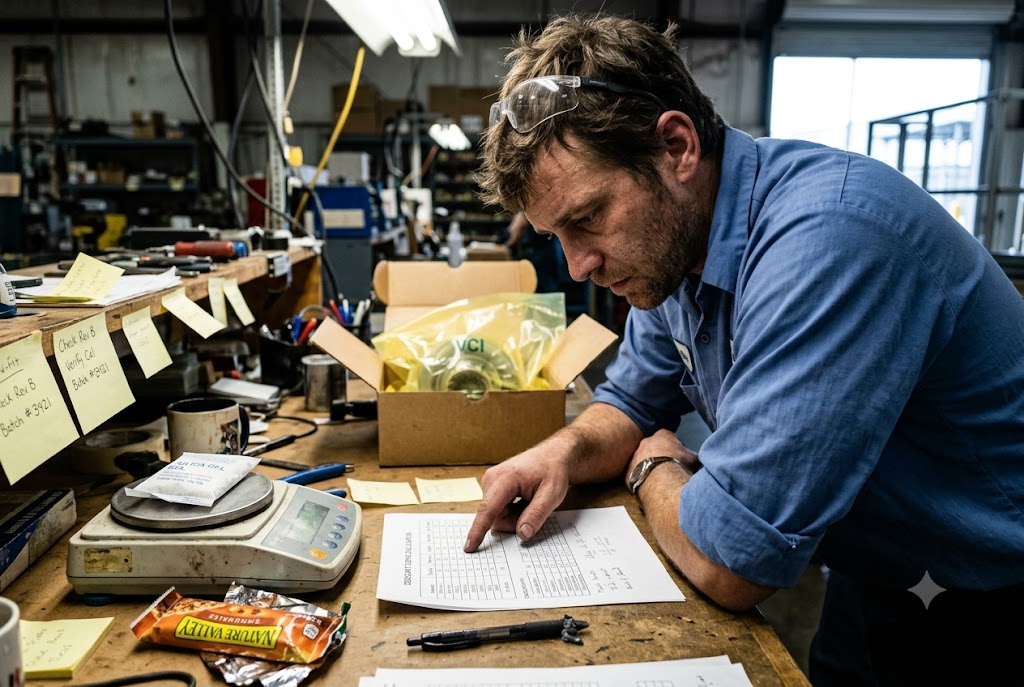
Specifying VCI bags at the shipment level is not enough. A master VCI bag over a bulk pile of loose EDM parts provides almost no protection to individual part surfaces, because metal-to-metal contact and abrasion break the inhibitor film exactly where the surface is most exposed. Precision EDM parts need individual protection before they go into any master container.
Contract language for individual wrapping should specify: each part wrapped separately in VCI film or interleaved with VCI tissue before placement in the master bag or carton, with no bare metal-to-metal contact permitted. Desiccant quantity should be calculated per the packaging volume and ambient conditions at origin, not specified as a fixed count per shipment.
Individual Wrapping Requirements by Part Type
Not every EDM part needs the same level of individual protection. The specification should be tiered based on part geometry and surface sensitivity.
| Part Category | Individual Wrapping Requirement |
|---|---|
| Flat plates and simple profiles | VCI tissue interleave, minimum one sheet per part |
| Complex 3D contour parts | Full VCI poly wrap, heat-sealed at part level |
| Hardened tool steel parts (D2, H13, M2 7) | Full VCI wrap + individual desiccant sachet, air-purged before sealing |
| Parts with blind features or deep keyways | Air-purge required; residual dielectric fluid must be removed before sealing |
| Tight-tolerance gauge-quality parts | Individual rigid tray or foam nest inside VCI wrap |
The hardened tool steel row deserves extra attention. Tool steels are more reactive after EDM because the heat-affected zone at the cut surface is different in chemistry from the parent metal. They also commonly have complex geometries — keyways, bores, internal profiles — that trap dielectric fluid. If that fluid is sealed inside a VCI bag, it off-gasses moisture throughout transit and can overwhelm the inhibitor's protective capacity.
Desiccant Sizing Language
Most contracts that mention desiccant at all say something like "1 silica gel 8 sachet per box." This is not engineering. Desiccant sizing depends on package volume, the humidity at the point of origin at time of packing, and the expected transit duration.
The standard reference for desiccant calculation is MIL-D-3464 9 or its commercial equivalent. You do not need to require full MIL compliance, but you can require that the supplier demonstrate their desiccant quantity is sized for the package volume and a 30-day transit in tropical origin conditions. Ask them to show the calculation. If they cannot, the specification is not being followed.
Contractual Enforcement Language
Here is a practical template for the relevant purchase order clause:
"Each part shall be individually wrapped in VCI film or interleaved with VCI tissue prior to placement in master packaging. No bare metal-to-metal contact is permitted within the shipping unit. Desiccant quantity shall be sized for package volume and 30-day transit duration in accordance with MIL-D-3464 or equivalent. Supplier shall document lot number, quantity, and desiccant type on the packing list."
This language is enforceable because it names the action, names the standard, and requires documentation. "Parts shall be rust-free" names only an outcome — and outcomes are disputed at destination, not at origin.
What Packaging Failures Cause the Most Transit Damage to Precision Wire EDM Machined Parts?
In my experience managing shipments across hundreds of EDM orders, the rust and damage we see at destination rarely comes from a single catastrophic failure. It comes from a sequence of small process shortcuts that compound over a 30-day ocean transit. Understanding the failure modes lets you write contract language that addresses causes, not just outcomes.
The most common transit damage causes for precision wire EDM parts are: staging parts on open racks after machining before packaging (exceeding the safe post-machining interval), using folded rather than heat-sealed VCI bags, omitting individual part separation, and failing to air-purge hardened steel parts with blind features before sealing.
The Post-Machining Interval Problem
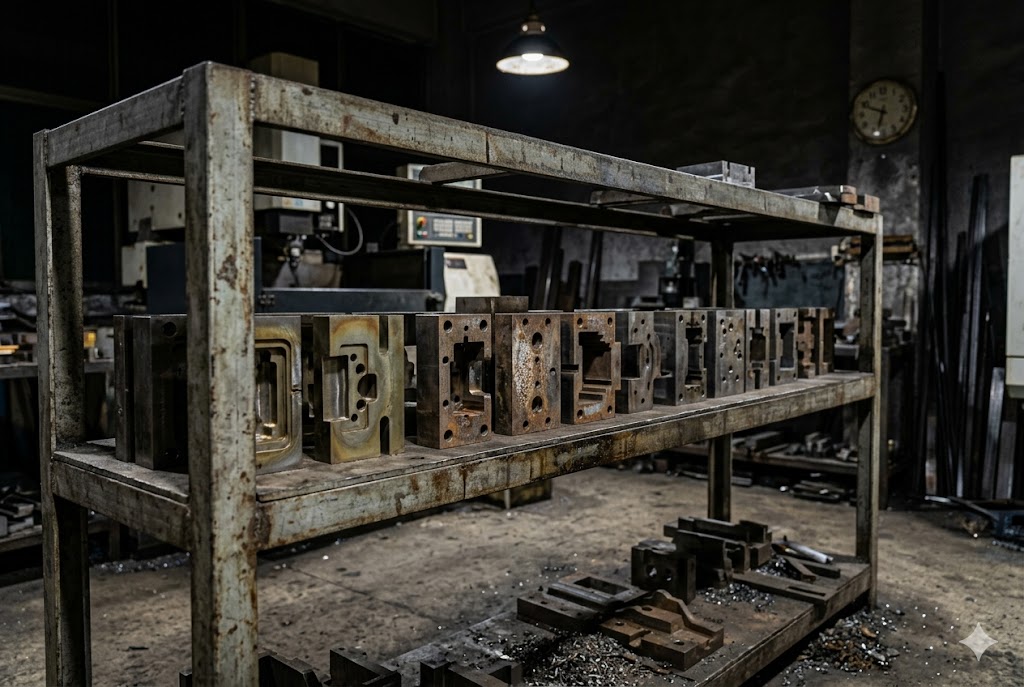
Many Chinese machine shops run wire EDM in batch mode. Parts come off the machine and get staged on an open rack until the full batch is complete — sometimes overnight. The fresh-cut surfaces begin oxidizing from the moment they leave the dielectric tank. By the time the batch is packaged, some parts may already have surface discoloration that passes visual inspection at low light but reveals itself as rust staining under proper inspection lighting at destination.
The fix is a contractual maximum post-machining-to-packaging interval. We specify ≤4 hours as our standard. The supplier must log the timestamp of part removal from the EDM tank and the timestamp of packaging seal for each lot. This sounds onerous, but any factory running a reasonable process control system can document this with minimal effort. Factories that resist this requirement often do so because they cannot meet the interval — which tells you something important about their process discipline.
Common Failure Mode Summary
| Failure Mode | Root Cause | Contract Countermeasure |
|---|---|---|
| Flash rust on cut surfaces at destination | Exceeded post-machining interval before packaging | Specify ≤4 hour interval, require timestamp log |
| Rust inside sealed bag | Folded closure instead of heat seal | Specify heat-seal only, prohibit folded closures |
| Surface corrosion at metal contact points | No individual part separation in master carton | Require individual VCI wrap or tissue interleave |
| Rust in blind features and bores | Residual dielectric fluid not removed before sealing | Require air-purge clause for complex geometries |
| Desiccant failure mid-transit | Undersized or wrong desiccant type | Require MIL-D-3464 sizing, silica gel or molecular sieve only |
| Container rain damage | Individual packages not sealed against condensation | Require heat-sealed individual and master packaging |
Why Visual Inspection at Source Does Not Catch This
This is the most important systemic point. Pre-shipment inspection 10 in China almost never involves opening sealed VCI packaging. An inspector who sees a properly heat-sealed VCI bag with a desiccant sachet visible through the film will typically record the packaging as compliant — and move on. They are not cutting open bags to check the part surface inside.
This means PSI is an incomplete control for rust prevention. It catches gross packaging failures — missing bags, wrong material, obvious damage. It does not catch parts that were staged too long before packaging, or bags that were heat-sealed over parts with residual moisture in blind features.
Your contract must account for this inspection gap. The cleanest way is to make the supplier responsible for rust-on-arrival within 30 days of delivery, regardless of PSI sign-off. This places the incentive correctly: the supplier must prevent the failure, not just pass the visual check.
Should Packaging and Rust Prevention Compliance Be Verified at Pre-Shipment Inspection?
Yes — but with a clear understanding of what PSI can and cannot verify. PSI is a useful control point for packaging compliance, but it must be scoped correctly to add value. If you send an inspector to check VCI bags without telling them exactly what to look for, you will get a pass/fail result based on visual format only. That is not sufficient for precision EDM parts.
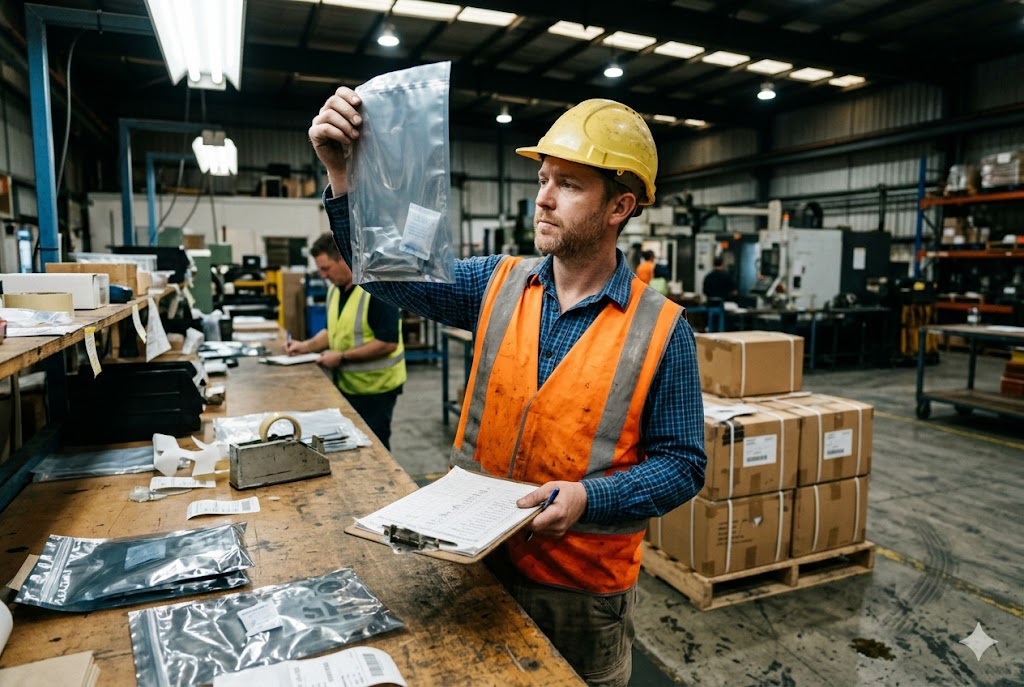
Packaging and rust prevention compliance should be included in every PSI scope for wire EDM parts, with specific checkpoints for VCI bag format, heat-seal integrity, desiccant presence, individual wrapping compliance, and photo documentation of sealed packages. PSI should be treated as a process audit checkpoint, not a final acceptance gate for rust.
What to Include in the PSI Scope
Give your inspection agency or internal inspector a written checklist. Verbal instructions produce inconsistent results. The checklist should cover the following:
| Inspection Item | Verification Method | Acceptance Criterion |
|---|---|---|
| VCI bag material | Check product label or supplier certificate | Nitrite-free, amine-free formulation confirmed |
| Seal method | Visual inspection of each package | Heat seal only — folded closures are rejection |
| Desiccant present | Visual through film before sealing, or open sample | Sachet visible inside sealed package |
| Individual part separation | Open sample master carton | No bare metal-to-metal contact in any unit |
| Packaging timestamp records | Review production log | Post-machining-to-seal interval ≤4 hours per lot |
| Photo documentation | Review submitted photos | Part number label visible inside bag before sealing |
The Photo Documentation Requirement
Require the supplier to photograph each lot's packaging before sealing, with a visible part number or lot tag inside the bag. This is a low-cost requirement that creates high-value evidence. When a buyer receives rust-damaged parts and the supplier claims "packaging was correct," the absence of pre-seal photos is itself evidence of non-compliance. When photos exist and show correct packaging, they help resolve liability disputes quickly.
This requirement also changes supplier behavior at origin. A team that knows they must photograph packaging before sealing is less likely to rush the process or substitute materials, because the photo record would show the substitution.
Using Final Payment as a Compliance Lever
The most effective contractual enforcement mechanism for packaging compliance is tying final payment release — or a payment holdback — to satisfactory receipt condition. Specifically: include a clause stating that rust, corrosion staining, or packaging non-conformance identified within 30 days of arrival constitutes a supplier-caused defect, and that the supplier is liable for replacement, rework, or a negotiated credit regardless of PSI outcome.
This clause changes the supplier's risk calculation. When the supplier knows that PSI sign-off does not extinguish their liability, they have a direct financial incentive to execute packaging correctly — not just to pass the visual check.
Conclusion
Rust on wire EDM parts is a contract problem before it is a chemistry problem. Write specific packaging requirements into every purchase order — VCI format, heat seal, desiccant sizing, individual wrapping, timestamp logs, photo records, and a receipt-condition liability clause. Vague language protects no one.
Footnotes
1. Detailed breakdown of typical sea freight transit times and routes from China to U.S. ports. ↩︎
2. Explains how deionized water functions as dielectric fluid during the wire EDM cutting process. ↩︎
3. Defines how oxide layers form on metal surfaces and protect against corrosion. ↩︎
4. Explains how vapor corrosion inhibitor technology forms a protective shield on metal surfaces. ↩︎
5. Describes how condensation forms inside shipping containers and damages cargo during transit. ↩︎
6. Best practices for sealing VCI packaging to maintain corrosion protection during shipment. ↩︎
7. Comprehensive guide comparing tool steel grades, including D2, H13, and M2 properties. ↩︎
8. Explains how silica gel desiccants absorb and release moisture inside sealed packaging. ↩︎
9. Full text of the military specification covering activated, bagged desiccants for packaging use. ↩︎
10. Explains what pre-shipment inspections in China cover and how they're conducted. ↩︎



