 Skip to main content Skip to footer

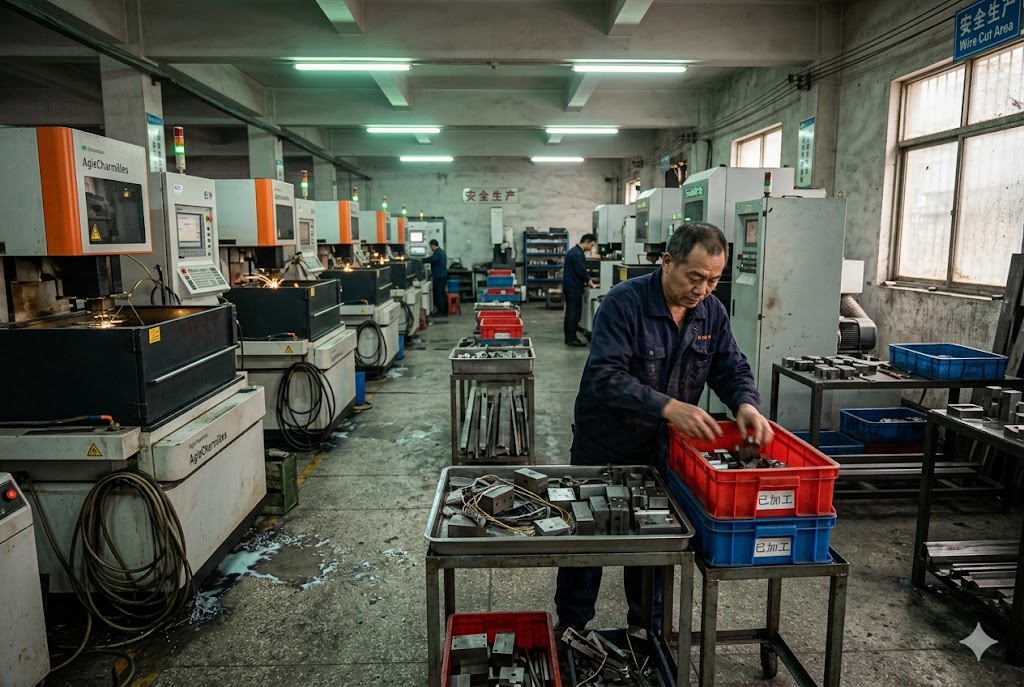
At our wire EDM workshop, we get this question from US buyers almost every week. Many assume coating happens under one roof. The truth often surprises them.
Most dedicated wire EDM factories in China do not run in-house surface treatment lines. Plating, anodizing, and passivation need separate wastewater systems and permits, so EDM shops send parts to outside coating partners. Your factory likely coordinates this work rather than performing it directly.
Let's look at what this means for your orders, your contracts, and your quality checks.
How Does Outsourced Surface Treatment Affect Lead Time and Quality Control Accountability?
In our years exporting custom parts, we have seen outsourced coating add hidden days to a schedule. It also blurs who owns a defect.
Outsourcing surface treatment adds extra transport time between the machining factory and the coating shop, often two to five days each way. It also creates a gap in accountability, because the machining factory may blame the coating shop for defects, and the coating shop has no direct contract with you.
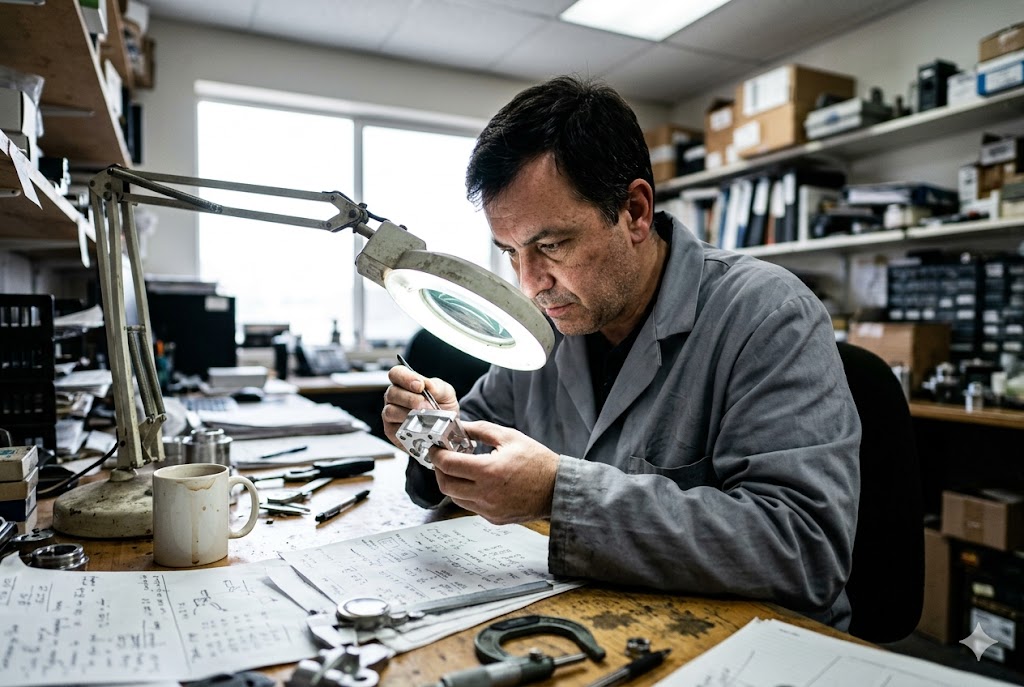
Most wire EDM shops focus on one job: cutting metal to a precise shape. Plating tanks, anodizing baths, and passivation lines need their own permits and wastewater treatment systems 1. Few factories want that extra cost and risk. So they send parts to a partner shop nearby.
This step adds time. The EDM factory must pack and ship parts to the coating shop. The coating shop must queue the job, run the process, then ship parts back. Each trip can take two to five days. If the coating shop is busy, your order waits in line behind other clients.
Why Lead Time Grows
Transport between factories is the biggest hidden delay. Add in queue time at the coating shop, and a "two week" job can stretch to three or four weeks. Weather, holidays, and traffic in Chinese industrial zones also play a role.
Who Is Responsible When Something Goes Wrong
When a finished part fails inspection, the machining factory may say the coating shop caused the problem. The coating shop has no contract with you, so they answer only to the machining factory. This makes it hard for you to get a fast fix or fair compensation.
| Factor | In-House Finishing | Outsourced Finishing |
|---|---|---|
| Lead time impact | Low, work runs in parallel | High, adds transport and queue time |
| Quality accountability | Clear, one factory owns the result | Split between two factories |
| Cost to you | Often higher base price | Often lower base price, hidden delays |
| Process visibility | Easy to inspect on site | Hard to inspect without extra trips |
A clear contract that names the finishing partner, sets a deadline for that step, and makes your main supplier responsible for the result can close most of this gap. We have found that buyers who write these details into the purchase order see far fewer disputes when a coating defect appears later. A simple line stating that the main supplier remains fully responsible for the finishing step, no matter who performs it, removes most of the confusion we described above. This single sentence can save weeks of back-and-forth emails when something does not look right.
Should I Require My Supplier to Disclose All Subcontractors for Surface Treatment?
Our sales team has learned that buyers rarely ask this question early enough. By the time they do, the coating shop has already changed twice.
Yes, you should require your supplier to name every surface treatment subcontractor in writing. This protects you because lot-to-lot quality, plating thickness, and salt spray performance can change when a factory swaps coating shops without telling you, even mid-order.
In our experience working with US buyers, the drawing spec is only half the story. A drawing might call for passivation per ASTM A967 2 or hard anodize per MIL-A-8625 Type III 3. But the contract rarely says who must perform that step, or that the spec must follow the part to the sub-tier shop.
China's coating industry is large but fragmented. Many small shops compete on price and speed. A machining factory may send parts to shop A this month and shop B next month, based on who has open capacity. Each shop may run slightly different process parameters.
What Disclosure Should Cover
A disclosure clause should ask for the name, address, and process certifications of any finishing subcontractor. It should also require written notice before any change, and your approval before that change takes effect.
What Happens Without Disclosure
Without this clause, you may receive parts from three different coating shops across one order, with no record of which batch went where. If a failure shows up later, tracing the cause becomes very hard.
| Disclosure Item | Why It Matters |
|---|---|
| Subcontractor name and location | Lets you check certifications and history |
| Process spec used | Confirms it matches your drawing requirement |
| Approval before change | Stops silent swaps mid-order |
| Batch traceability | Helps trace defects back to a specific shop |
We always recommend writing this into the purchase order, not just discussing it by email, so it is enforceable if something goes wrong. In practice, we keep a simple supplier list for every client, showing which finishing shop handled each batch. This list takes only a few minutes to update, but it gives both sides a clear record. When a buyer asks for this list before placing an order, it also signals that quality control is a real priority, not just a checkbox.
Can I Audit the Coating Subcontractor Directly if the Surface Treatment Is Critical?
When we manage critical orders for clients, we sometimes arrange a direct visit to the coating shop. Most buyers do not know this option exists.
Yes, you can audit a coating subcontractor directly, but only with your main supplier's agreement and presence. A direct audit lets you check coating thickness, adhesion, salt spray testing, and passivation results against your drawing specs before parts ship.
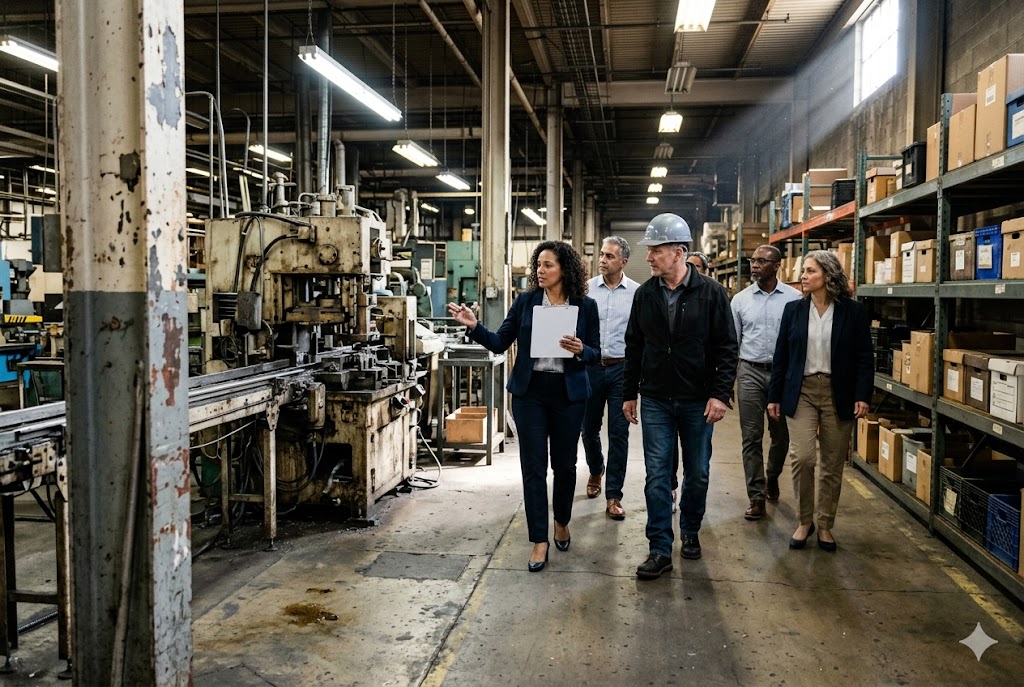
From our project management work, an audit is most useful for parts going into safety, aerospace, or medical applications. For these jobs, a coating that looks fine to the eye can still fail a salt spray test or have poor adhesion.
What a Coating Audit Should Check
A real audit goes beyond a factory tour. It should include measurement of coating thickness using XRF 4, a cross-hatch adhesion test per ASTM D3359 5, and salt spray testing per ASTM B117 6 for corrosion resistance. For passivated stainless steel, a ferroxyl or copper sulfate test per ASTM A380 7 confirms free iron has been removed.
Working Through Your Main Supplier
Most coating shops will not let an outside buyer walk in alone. Your main supplier usually needs to arrange the visit, send their quality staff with you, and confirm the relationship. A good supplier with a managed network of certified finishing partners will not resist this request.
| Audit Item | Standard Used | What It Confirms |
|---|---|---|
| Coating thickness | XRF measurement | Matches drawing tolerance |
| Adhesion | ASTM D3359 | Coating will not peel or flake |
| Corrosion resistance | ASTM B117 salt spray | Coating survives expected exposure |
| Passivation check | ASTM A380 | Free iron removed from surface |
If your supplier resists a basic audit request, or cannot tell you which shop handles your parts, that is a warning sign. A confident supplier will treat your request as normal, not as a threat. We also suggest scheduling these audits before mass production starts, not after parts have already shipped. A pre-production audit lets both sides agree on acceptable results using a real sample, which becomes the reference point for every batch that follows. This step costs a little time upfront but saves much more time later.
Does Outsourcing Anodizing or Plating Increase the Risk of Dimensional Non-Conformance?
On our shop floor, we plan EDM cuts around the final coating thickness. When that coating step moves outside our walls, this planning gets harder to control.
Yes, outsourcing anodizing or plating can raise the risk of dimensional non-conformance. Coatings like electroless nickel add thickness to every surface, so the EDM program must remove that extra material in advance. If the coating shop changes, this allowance can be lost.
In our tooling department, we treat coating thickness as part of the dimensional spec, not an extra step added later. For example, electroless nickel 8 typically adds about 0.0001 to 0.0003 inches per surface. On a part with single-digit micron tolerances, this is not a small number.
Why Material and Process Choices Matter
The raw EDM finish also depends on the base material. Hardened tool steels with an even grain cut very smoothly, while untreated aluminum often stays around 39 microinches Ra. EDM can also leave a thin recast layer on the cut edge, which some specs require to be removed by electropolishing before plating 9 even begins.
How a Coating Shop Change Causes Problems
If the coating shop changes between orders, the new shop may apply a slightly different thickness, even within the same spec range. If the EDM program was set for the old shop's typical thickness, the final part may now sit outside tolerance after coating.
| Step | Risk If Coating Shop Changes |
|---|---|
| EDM pre-coat sizing | May no longer match new coating thickness |
| Recast layer removal | May be skipped or done differently |
| Final dimension check | May fail tolerance after plating |
| Process documentation | May not match original approved sample |
To avoid this, the coating allowance should be written on the drawing, and any change of coating shop should trigger a new first-article inspection 10 before full production continues. We always recommend keeping a record of the exact coating thickness used on the approved first article, then comparing every new batch against that number. Even small shifts, such as moving from 0.0002 to 0.00035 inches, can push a tight-tolerance part out of spec. A short measurement check at receiving can catch this before parts reach your customer.
Conclusion
Surface treatment is usually outsourced, even when your supplier does not say so. Ask for disclosure, request audits, and lock coating allowances into your drawings.
Footnotes
1. EPA rules covering wastewater discharge limits and permitting for electroplating and metal finishing operations. ↩︎
2. Overview of the ASTM A967 standard governing chemical passivation treatments for stainless steel parts. ↩︎
3. Reference guide explaining MIL-A-8625 anodic coating types, including Type III hardcoat anodizing. ↩︎
4. Explanation of how handheld XRF analyzers measure metal coating thickness non-destructively. ↩︎
5. Step-by-step guide to performing the ASTM D3359 cross-hatch coating adhesion test. ↩︎
6. Details on ASTM B117 salt spray testing for evaluating coating corrosion resistance. ↩︎
7. Overview of ASTM A380 cleaning, descaling, and passivation practices, including the ferroxyl test. ↩︎
8. Guide to electroless nickel plating benefits and dimensional considerations for machined parts. ↩︎
9. How electropolishing removes the recast layer left by wire EDM before coating. ↩︎
10. Background on first article inspection as a quality verification step before production. ↩︎



