 Skip to main content Skip to footer

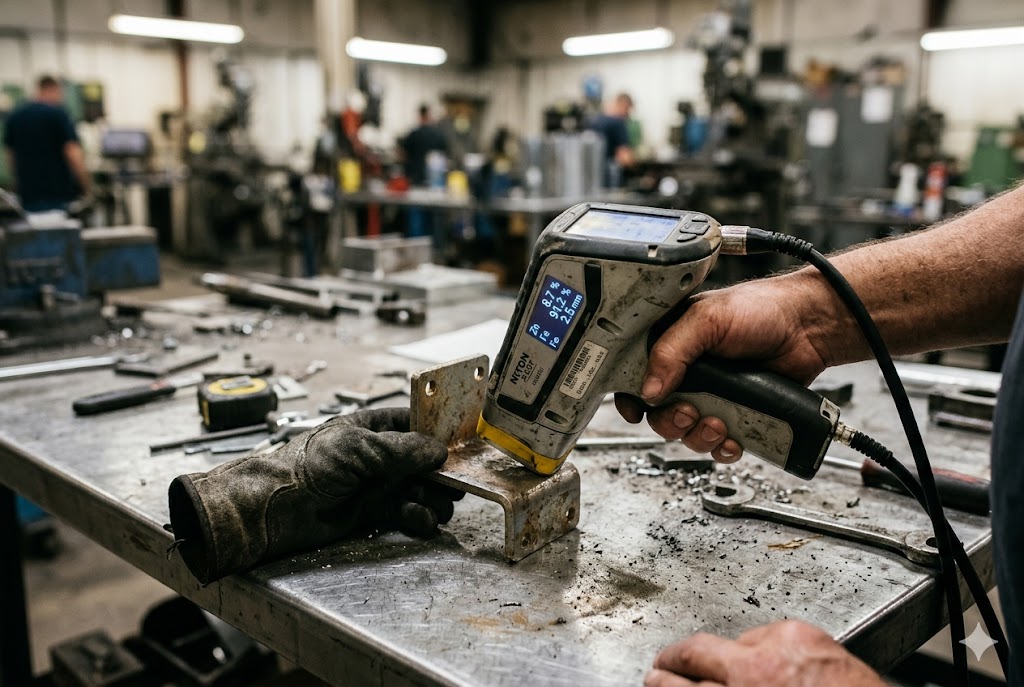
We have rejected more shipments over plating non-conformance than almost any other defect category. The parts look fine. The supplier says the COC is attached. But once our team runs an XRF instrument on-site, the numbers tell a different story.
Plating thickness verification requires selecting the right test method — XRF for non-destructive spot checks, cross-section metallography for disputes, and magnetic or eddy current gauges for production-line use. The correct method depends on the substrate, coating type, and whether the inspection is pre-shipment or incoming.
Each method has a specific application window. Choosing the wrong one at the wrong stage costs time, money, and leverage when a dispute reaches arbitration.
What Instrument Measures Electroplating Thickness on Wire EDM Machined Parts?
Our quality team handles parts from wire EDM operations 1 regularly, and the question of which gauge to reach for is not always obvious.
For wire EDM machined parts, XRF (X-ray fluorescence per ASTM B568) is the primary non-destructive choice. It measures both thickness and elemental composition simultaneously, making it effective for detecting substituted or diluted plating materials without cutting into the part.
Why Wire EDM Parts Complicate Thickness Measurement
Wire EDM produces very tight-tolerance surfaces. These parts often have fine recesses, small bores, and sharp internal corners. Standard magnetic gauges struggle with these geometries. The probe needs a flat, accessible surface to get a valid reading.
XRF does not have the same geometric sensitivity. It fires an X-ray beam at the surface and reads the fluorescence response from the coating and substrate. As long as the beam can reach the surface, it returns a valid result.
Test Method Comparison for EDM Parts
| Method | Standard | Destructive | Best For | Limitations |
|---|---|---|---|---|
| XRF | ASTM B568 | No | Multi-layer, precious metals, composition check | Requires flat or accessible surface |
| Magnetic | ASTM B499 | No | Zn, Cd, Cr on steel | Cannot use for Ni on steel |
| Eddy Current | ASTM B244 | No | Anodize on aluminum | Nonmagnetic conductive substrates only |
| Cross-Section / Metallography | ASTM B487 | Yes | Dispute resolution, void detection | Destroys the sample |
When Magnetic and Eddy Current Methods Still Apply
The magnetic method (ASTM B499) 2 works well for zinc, cadmium, or chrome coatings on steel substrates. It is fast, non-destructive, and suitable for SPC applications on a production floor. One hard rule: do not use it for electrodeposited nickel on steel. The magnetic permeability of nickel interferes with the measurement, and the result will be unreliable.
The eddy current method (ASTM B244) 3 is the correct choice for anodize on aluminum. The coating acts as a spacer between the probe and the conductive substrate. The instrument reads the impedance change and calculates thickness from that delta.
Destructive Cross-Section Testing
ASTM B487 4 is the referee method. A coated specimen is sectioned, polished, and examined under a metallographic microscope. This gives you actual deposited thickness, uniformity across the cross-section, and visibility of discontinuities, voids, or inclusions. It is the most legally defensible result if a dispute escalates to CIETAC arbitration 5. You will destroy the part, but you will know exactly what was deposited.
For multilayer plating systems — for example, copper strike plus nickel plus chrome — surface XRF alone may not be sufficient. The instrument's penetration depth varies by layer density and order. If you have a known layer sequence and expected thickness range, XRF can work. If those parameters are unknown or the layers are thin and dense, cross-section metallography is the definitive answer.
Should Coating Thickness Be Verified at Pre-Shipment Inspection or at My Facility on Arrival?
We have seen this question come up in almost every client conversation where plated parts are involved.
Coating thickness must be verified at pre-shipment inspection, on-site at the plater or plating sub-supplier, using a calibrated instrument. Inspecting at your facility on arrival is too late — once parts are shipped and commingled with compliant inventory, remediation options are destructive and expensive.
Why Location of Inspection Matters
Pre-shipment inspection (PSI) at the plating facility gives you real options. If the XRF reading shows the coating is 30% below the minimum callout, you can reject the lot before it ships. The plater can re-plate or replace. No freight has been wasted. No downstream production line has been disrupted.
If you wait until arrival at your warehouse, the situation is different. Parts may be mixed with other lots. A full sort is required. Destructive sampling on an AQL plan is your only verification option, and that plan must already exist in your purchase order to be enforceable.
What a Good PSI Plating Check Covers
| Inspection Item | Why It Matters |
|---|---|
| XRF on representative sample | Actual coating thickness at accessible locations |
| Critical location callout check | Bores, recesses, edges — not just flat faces |
| Pre-plate vs. post-plate dimensional delta | Confirms no fit interference from coating buildup |
| COC review — instrument, calibration, measurement locations | Distinguishes real data from a blanket conformance statement |
| Visual for blistering, pitting, uncoated patches | Detects adhesion failures or masking errors |
The Commingling Problem
Once a non-conforming lot ships and arrives at a distribution point, it is nearly impossible to segregate without 100% destructive testing. You cannot visually distinguish an 8 µm nickel coating from a 5 µm nickel coating. They look identical. The only recovery path is cross-section sampling on a statistically valid plan — which destroys parts and extends lead times.
Define your AQL level and sampling plan 6 contractually, before the first production run. Tie it to your drawing thickness callout. If the drawing says "8 µm min," the PO should reference that callout and name the AQL level and test method. That language is what gives you enforceable rejection authority.
Calibration Traceability Is Not Optional
Any XRF instrument used for acceptance testing must have a current calibration certificate traceable to a national metrology standard 7. Ask to see it before the inspection begins. An uncalibrated instrument produces data that cannot be used for rejection or dispute purposes. This applies to third-party inspection agencies as well as in-house QC teams.
How Many Measurement Points Per Part Are Needed to Confirm Uniform Coating Thickness?
There is no single universal number. What matters is where you measure and why.
The number of measurement points per part depends on part geometry, critical functional surfaces, and the plating process used. For flat simple parts, five points in a cross pattern is a standard minimum. Complex geometry — bores, recesses, threaded features — requires additional points at each critical location explicitly called out on the drawing.
Flat Parts vs. Complex Geometry
Electrolytic plating deposits unevenly. Current density drives deposition, so outside corners and raised features receive more coating than recesses and internal bores. A part that reads 12 µm on its flat face may have 4 µm in a blind bore two centimeters deep.
Electroless nickel (EN) is the exception. EN deposits by chemical reaction, not current, so thickness distribution is nearly uniform across complex geometry. For EN-coated parts, fewer measurement points may be statistically sufficient. For electrolytic zinc, chrome, or copper, you need points at the geometrically challenging locations.
Measurement Point Guidelines by Part Type
| Part Type | Minimum Points | Critical Locations to Include |
|---|---|---|
| Flat plate or simple prismatic | 5 (cross pattern) | All four corners and center |
| Turned/cylindrical part | 4 (at 90° intervals) + 2 end faces | Threads, undercuts, OD face |
| Parts with bores | 5 standard + 1 per bore | Bore entry, mid-bore, bore exit |
| Parts with recesses or pockets | 5 standard + 1 per recess | Bottom of recess, recess walls |
| Threaded features | 2 per threaded zone | Root and crest if accessible |
Drawing Callout Defines Your Measurement Obligation
A blanket drawing callout — "Zn plating per ASTM B633, 8 µm min" — does not obligate the plater to achieve that thickness in difficult-to-plate geometry. If a bore or recess is functionally critical and requires a minimum coating, that location must be explicitly called out on the drawing, with a stated minimum for that feature.
This is a design responsibility, not a supplier responsibility. Without an explicit callout, the supplier is only obligated to meet the blanket spec on accessible surfaces. If your QC plan requires measurements at internal bores, write it into both the drawing and the PO.
Statistical Sampling vs. 100% Measurement
For high-volume runs, 100% XRF measurement is impractical. Define a sampling plan by lot size. The plan should reference a specific AQL level. A common approach for plating verification is to tie sampling to your incoming inspection AQL for dimensional features — typically AQL 1.0 for critical dimensions, AQL 2.5 for major features. If any sample point fails, the entire lot is quarantined pending further evaluation.
What Coating Thickness Deviation Is Acceptable Before I Can Formally Reject a Shipment?
This is where most disputes start. The answer is contractual, not technical.
Formal rejection authority is established by drawing callout language, PO terms, and the referenced test standard. If the drawing specifies "X µm min," any measurement below that value on a sampled part within your AQL plan is a valid basis for rejection. Ambiguous callouts — nominal values without a stated minimum — give the supplier room to negotiate.
Drawing Callout Language Controls Everything
Chinese platers interpret ambiguous callouts as nominal targets. If your drawing says "8 µm nickel," a supplier in Dongguan reads that as a target, not a floor. They will deliver parts at 7.5 µm and call it acceptable. Without an explicit minimum, they are not wrong under standard interpretation.
Always write callouts as minimums with an upper bound when dimensional stack-up matters. For example: "Electroless nickel per ASTM B733 8, Type IV, 10 µm min / 15 µm max." That language creates an unambiguous acceptance window. Anything below 10 µm is a non-conformance. Anything above 15 µm may cause fit interference in an assembled product.
What Makes a Rejection Formally Enforceable
| Requirement | Why It Matters |
|---|---|
| Drawing callout states "X µm min" | Establishes the acceptance floor unambiguously |
| PO references drawing revision | Ties the callout to the contractual document |
| Named test method (e.g. ASTM B568 9) | Defines how measurement is performed and disputed |
| Calibration traceability on inspection instrument | Makes measurement data defensible in arbitration |
| Sampling plan with AQL level defined pre-production | Establishes how many failures constitute lot rejection |
| Measurement locations documented | Shows that critical features were tested, not just flat faces |
The COC Is Not Sufficient on Its Own
Suppliers routinely provide a Certificate of Conformance that states "coating meets drawing requirements." This document means nothing on its own. A valid COC must reference the specific ASTM or MIL-SPEC test method used, name the instrument and its calibration certificate, state the sample size, list the measurement locations, and record the actual measured values — not a blanket conformance statement.
If the COC says "meets drawing" without data, and your XRF readings show parts below minimum on arrival, the supplier will dispute your findings. A data-backed COC at the time of shipment creates a paper trail that supports your rejection and limits the supplier's ability to claim the defect occurred during transit.
Pre/Post Dimensional Delta for Tight-Tolerance Parts
Plating adds material. For parts with tight clearance or interference fits, the added thickness must be accounted for. Our team always requires pre-plate and post-plate dimensional inspection at the same datums and features for any part with a fit tolerance tighter than H7/g6. If the supplier only measures post-plate, you cannot determine whether the part was in-tolerance before coating — and a plating-induced dimensional failure is not the same claim as a plating-thickness failure.
Electroless nickel is particularly important here. EN deposits at near-uniform thickness, meaning the entire surface grows by the coating amount. A 12 µm EN coating adds approximately 0.012 mm to every feature. If a bore is 0.010 mm from maximum material condition before plating, it will be out of tolerance after.
Conclusion
Plating verification is a process problem, not just an incoming inspection problem. The right instrument, the right callout language, the right inspection stage, and the right COC format all need to be defined before production starts — not after parts arrive with the wrong thickness.
Footnotes
1. Overview of wire EDM precision machining and the tolerances it can hold. ↩︎
2. ASTM B499 standard for magnetic coating thickness measurement on steel. ↩︎
3. ASTM B244 standard for eddy current measurement of anodize on aluminum. ↩︎
4. ASTM B487 standard for cross-section metallography coating thickness verification. ↩︎
5. Overview of CIETAC arbitration rules for resolving China-related trade disputes. ↩︎
6. ANSI/ASQ Z1.4 standard defining AQL sampling plans for inspection. ↩︎
7. NIST explanation of measurement traceability and calibration certification. ↩︎
8. ASTM B733 specification for autocatalytic electroless nickel-phosphorus coatings. ↩︎
9. ASTM B568 standard for measuring coating thickness by X-ray spectrometry. ↩︎



