 Skip to main content Skip to footer

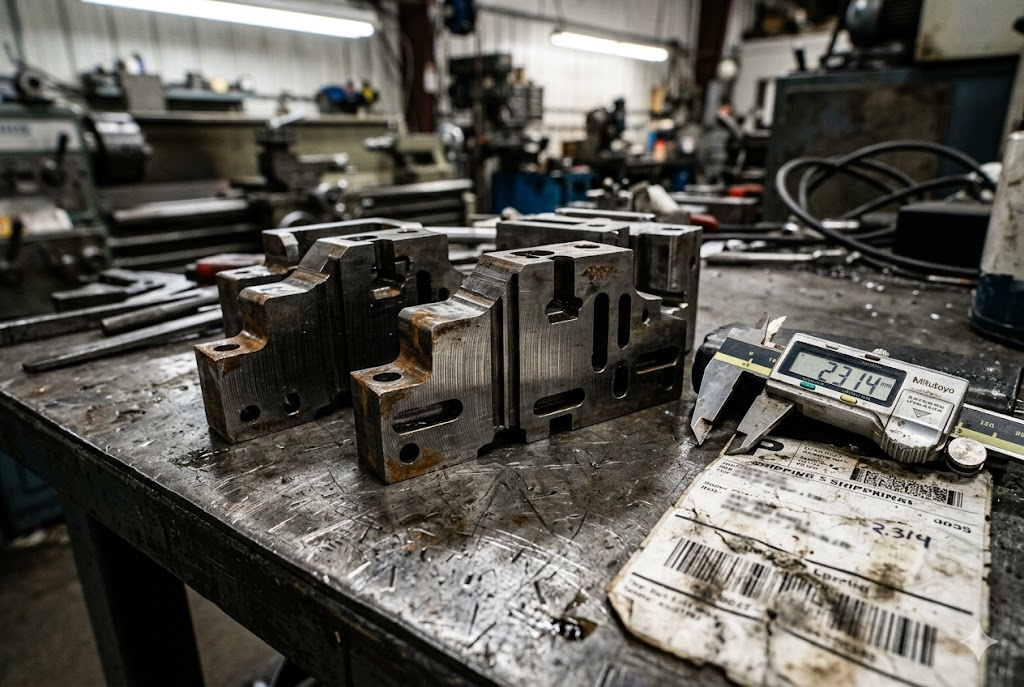
We have seen too many shipments arrive with a single line on the packing list: "Material: D2 tool steel. Heat treated." No report. No data. No traceability. When a buyer pushes back, the supplier sends a material cert from the steel distributor — which tells you nothing about what happened in the furnace or on the EDM machine.
To require a hardness test report from your supplier for wire EDM parts, you must anchor the requirement in three places: the engineering drawing, the purchase order quality clause, and a supplier quality requirements document. Verbal requests and email reminders are not enforceable. Written contractual language is.
The sections below break this down step by step. Each one covers a specific piece of the puzzle — method selection, sampling, traceability, and rejection criteria.
Which Hardness Test Method — Rockwell, Vickers, or Brinell — Is Appropriate for My Parts?
Our team runs into this question on almost every new part quote for heat-treated tool steel. The wrong method produces a number that looks legitimate but means nothing for your application.
For most wire EDM parts made from hardened tool steels such as D2, H13, A2, or M2, Rockwell HRC per ASTM E18 is the standard bulk hardness method. Vickers HV per ASTM E384 is required for thin sections, coatings, or near-surface recast layer inspection. Brinell HB is rarely appropriate for wire EDM parts.
Why Method Selection Matters
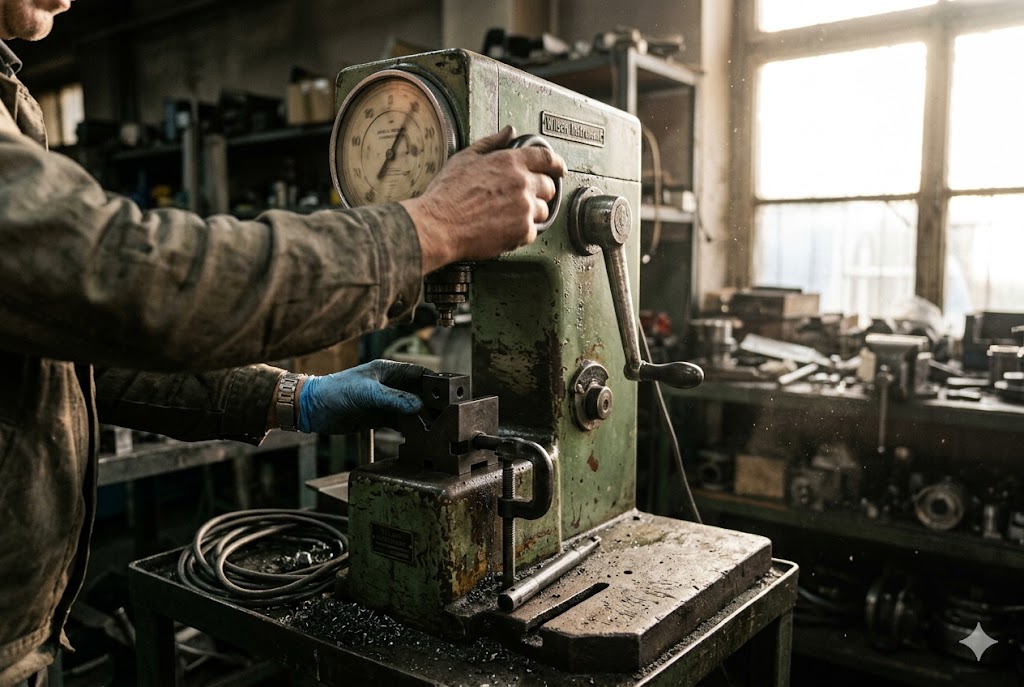
Each test method works differently. Rockwell hardness testing 1 uses a diamond cone indenter and measures depth of penetration under load. It is fast, repeatable, and widely available in Chinese machine shops. Vickers uses a square pyramid indenter and measures the diagonal of the indentation under a microscope. It is slower but far more precise for small features and thin cross-sections.
Wire EDM creates a recast layer with microcracks 2 — sometimes called a white layer — on every cut surface. This layer is 2 to 15 µm thick. It is harder and more brittle than the base metal. A Rockwell test cannot measure something that thin. You need Vickers microhardness testing 3 if you care about that surface zone.
Method Selection by Part Type
| Part Characteristic | Recommended Method | Standard |
|---|---|---|
| Bulk hardened tool steel (D2, H13, A2, M2) | Rockwell HRC | ASTM E18 |
| Thin wall < 3 mm or small cross-section | Vickers HV | ASTM E384 |
| Near-surface / recast layer inspection | Vickers HV (microhardness) | ASTM E384 |
| Soft materials (aluminum, brass, mild steel) | Brinell HB testing 4 or Rockwell HRB | ASTM E10 / ASTM E18 |
| Case-hardened parts with thin case depth | Vickers HV | ASTM E384 |
What to Put on the Drawing
The drawing callout is your primary contractual anchor. A PO note alone is not sufficient — Chinese suppliers treat the drawing as the governing fabrication document. The callout should specify the method, scale, acceptance range, and applicable standard. Example:
60–62 HRC per ASTM E18, verify per lot, report required with shipment.
For recast layer control on fatigue-critical parts, add a second callout:
Surface microhardness ≤ 900 HV0.1 per ASTM E384, tested within 0.5 mm of EDM cut edge, 3 points minimum.
Do not write "hardness: 60 HRC" without a standard reference. The supplier will use whatever tester is available and report whatever result comes out. For reference, D2 tool steel typically hardens to a range of 58–62 HRC 5 depending on tempering temperature, while H13 hot work steel is commonly specified in the 44–52 HRC range 6.
The Recast Layer Problem
Wire EDM's spark erosion melts and re-solidifies a thin layer of metal on every cut face. This recast layer has a different microstructure from the base material. It can contain microcracks. For punch and die tooling, mold inserts, or any part that will see cyclic loading, this surface condition matters. A Rockwell test on the body of the part will not detect recast layer hardness anomalies. That is why Vickers microhardness on the cut surface is a separate requirement, not a substitute for bulk testing.
Should Hardness Testing Be Performed on Every Part or on a Sample from Each Batch?
This is a cost and risk trade-off. We discuss it with clients before writing the quality clause into the PO, because the answer depends on part criticality, lot size, and the consequences of a missed nonconformance.
For most production wire EDM lots, 100% hardness testing is not required. An AQL-based sampling plan — such as AQL 1.0, Level II per ANSI/ASQ Z1.4 — provides statistically defensible coverage without adding excessive cost. Critical safety or tooling parts may justify tighter sampling or 100% inspection.
Why You Cannot Let the Supplier Decide
If your PO does not specify a sampling plan, the supplier will test one piece and report it as representative of the lot. That is common practice in Chinese EDM shops. For a batch of 200 parts from multiple heat treat cycles, testing one piece gives you almost no statistical confidence.
AQL Sampling Reference Table
| Lot Size | AQL 1.0, Level II — Min Sample Size | Accept / Reject Numbers |
|---|---|---|
| 2–8 | 2 | 0 / 1 |
| 9–15 | 3 | 0 / 1 |
| 16–25 | 5 | 0 / 1 |
| 26–50 | 8 | 0 / 1 |
| 51–90 | 13 | 0 / 1 |
| 91–150 | 20 | 0 / 1 |
| 151–280 | 32 | 1 / 2 |
| 281–500 | 50 | 1 / 2 |
Source: ANSI/ASQ Z1.4 sampling standard 7, Normal Inspection, AQL 1.0, Level II.
Witness Coupons and Furnace Lots
For heat-treated parts, hardness is a function of the furnace run — not the raw material. A single heat treat cycle may include 20, 50, or 200 parts. If those parts came from the same furnace load, testing a statistically valid sample from that load is defensible. But if your batch of 200 parts was heat-treated in four separate furnace runs, you need samples from each run — not just from the batch as a whole.
Specify this in your Supplier Quality Requirements document:
Hardness testing must be performed on a minimum of one finished part or witness coupon per furnace run. If a production lot spans multiple furnace runs, each run must be sampled independently.
When 100% Testing Makes Sense
| Scenario | Recommended Approach |
|---|---|
| Safety-critical tooling (aerospace, medical) | 100% hardness test, full traceability |
| First article / new supplier qualification | 100% on the first lot |
| Prior nonconformance history with this supplier | 100% until three clean lots |
| Low-volume prototype (1–5 parts) | 100% (cost impact is minimal) |
| Standard production, established supplier | AQL 1.0, Level II per ANSI/ASQ Z1.4 |
How Do I Verify That the Hardness Report Reflects the Actual Parts Being Shipped to Me?
This is the most common gap we find when auditing Chinese EDM suppliers. The report exists. The numbers pass. But the test was done on raw bar stock before machining — or on a sample part from a previous order. The numbers on the certificate have no relationship to the parts in the box.
To verify that a hardness test report reflects the actual shipped parts, require that the report reference the specific production lot number, heat treat batch ID, furnace run date, and part serial or tag numbers. The test date must fall after EDM completion — not before. Calibration traceability must be documented on the same report.
What a Valid Hardness Test Report Must Contain
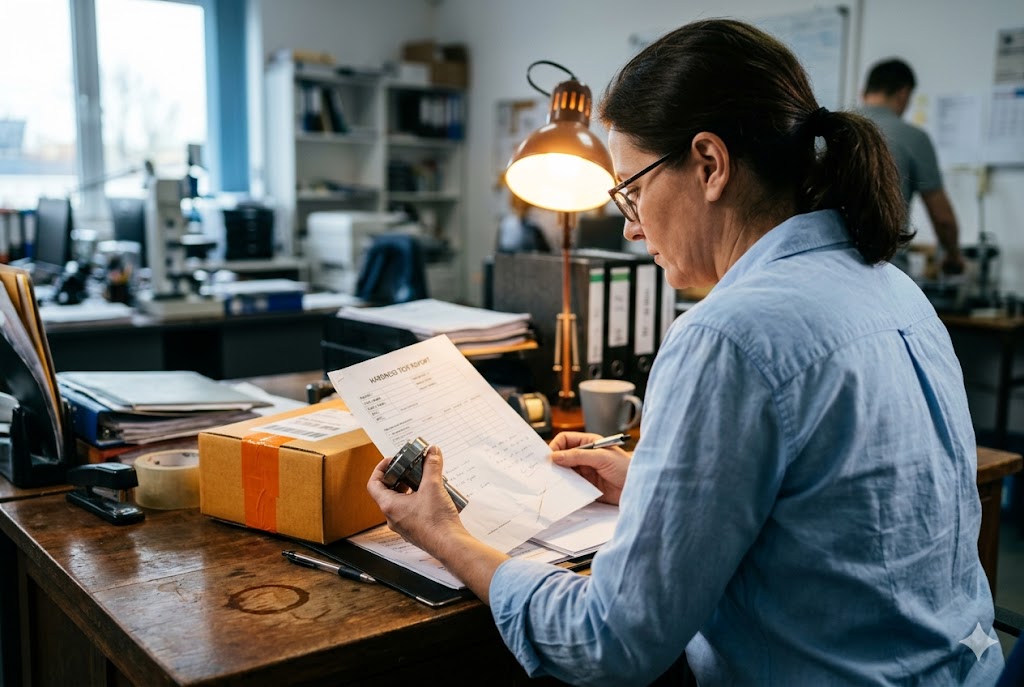
A compliant report is not a number on a page with a stamp. It is a traceable document. When we review supplier reports for clients, we check for all of the following fields. If any are missing, we send it back.
| Required Field | What to Look For |
|---|---|
| Test method and scale | "Rockwell HRC per ASTM E18" — not just "HRC" |
| Applicable standard | ASTM E18, ASTM E10, or ASTM E384 |
| Number of test points | Minimum 3 points per part or coupon |
| Test point locations | Described or shown on a sketch |
| Actual measured values | Individual readings, not just an average |
| Acceptance range | The drawing requirement stated explicitly |
| Pass/Fail conclusion | Stated against the drawing requirement |
| Lot number / job number | Must match the shipping documents |
| Heat treat batch ID | Must reference the specific furnace run |
| Test date | Must be after EDM completion |
| Tester name and signature | QC personnel, not sales |
| Equipment ID | Hardness tester model and serial number |
| Calibration certificate number | Tester calibration reference |
| Calibration date | Must be current — within the tester's calibration interval |
| Calibration block value | The certified block used for daily verification |
The Pre-Machining Test Problem
Chinese EDM shops frequently test hardness on raw stock before machining. They then use that result as post-process conformance documentation. This is wrong for two reasons. First, heat treatment occurs after rough machining in many workflows — so the raw stock test predates the actual heat treat cycle. Second, even when heat treat occurs before EDM, the EDM thermal cycle in the HAZ can locally alter surface hardness.
Contractually counter this by specifying:
The hardness test must be performed on the finished machined part, or on a witness coupon processed in the same heat treat furnace run as the production parts. The QC stamp and test date must reflect completion after all EDM operations.
Calibration Traceability
Hardness testers in Chinese machine shops are often calibrated infrequently. A tester with a worn indenter or a drift in the load cell will produce consistently false readings — all of which will appear to pass. Require the report to cite:
- The tester's calibration certificate number
- Calibration date
- The certified hardness value of the calibration block used for daily verification
- Traceability to a national metrology standard (NIST or equivalent such as CNAS in China 8)
Without this, the numbers on the report are unverifiable.
Third-Party Verification Right
Include a clause in your PO or SQR that gives you the right to appoint an independent inspector — SGS, Bureau Veritas, or Intertek 9, or your own representative — to conduct hardness verification on retained samples before or after shipment. Non-conformance found during third-party inspection should trigger supplier-paid re-inspection and quarantine of the affected lot.
What Hardness Deviation Triggers a Formal Rejection of a Heat-Treated Wire EDM Batch?
We set rejection thresholds with clients during the PO drafting stage — not after a nonconformance arrives. Waiting until parts fail to define "how far off is too far off" is a losing position. You need a number in the contract before the parts ship.
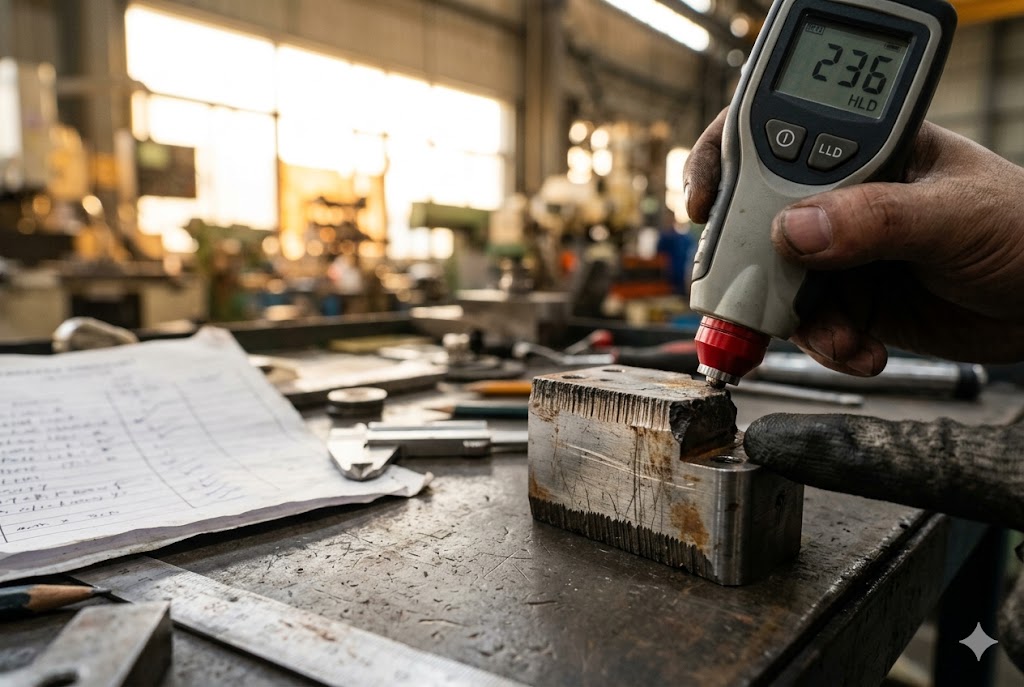
A formal rejection is triggered when any tested part or coupon from a heat-treated wire EDM lot falls outside the drawing-specified hardness range, or when the measured hardness deviation exceeds the supplier's stated tolerance — typically ±1 HRC from the nominal. Zero tolerance for out-of-range readings at AQL 1.0 is the standard contractual position.
Defining the Rejection Threshold in the Contract
The drawing callout defines the acceptance range. The quality clause defines what happens when a result falls outside that range. These are two separate documents and both are necessary. A drawing that says "62–65 HRC" without a quality clause leaves the rejection process undefined. The supplier may argue that one failed part out of fifty is acceptable. Without written language, you have no contractual basis to reject the lot.
Typical Rejection Thresholds by Application
| Application | Typical Hardness Range | Rejection Trigger |
|---|---|---|
| Punch and die tooling (D2) | 58–62 HRC | Any reading < 58 or > 64 HRC |
| Hot work tooling (H13) | 44–52 HRC | Any reading outside the range |
| Cold work tooling (A2) | 57–62 HRC | Any reading outside the range |
| High-speed steel tooling (M2) | 63–66 HRC | Any reading < 63 HRC |
| General precision fixtures | Per drawing ± 1 HRC | > 1 HRC deviation from nominal |
HAZ Softening at Cut Edges
Wire EDM's thermal cycling in the heat-affected zone 10 can soften the material locally — especially in tool steels heat-treated at the lower end of their specification window, or in materials with marginal hardenability. This softening may not show up in a bulk hardness test taken on the body of the part.
Specify in your SQR that hardness measurement must include points within 1–2 mm of major EDM cut edges on the finished part, not only on the body. This catches heat-affected zone softening that bulk testing alone would miss.
Disposition of Rejected Lots
When a lot is formally rejected, your quality clause should define the disposition path:
- Sort and re-test: Supplier 100% tests the remaining lot and segregates nonconforming pieces.
- Re-heat treat: If the material and geometry allow, rejected parts may be re-heat treated. Supplier must submit a new hardness report for the re-processed lot.
- Scrap and replace: For out-of-tolerance conditions that cannot be corrected by re-heat treatment, the lot is scrapped and replaced at supplier cost.
- Supplier-paid re-inspection: If third-party verification found the nonconformance, all re-inspection costs are charged to the supplier.
Define each of these options in your Supplier Quality Requirements document — and specify the decision authority. The buyer, not the supplier, decides which disposition path applies.
Conclusion
Getting a compliant hardness test report from a Chinese wire EDM supplier is not complicated — but it requires written requirements in three places: the drawing, the PO quality clause, and the SQR. Set the standards before the parts go into production, and you will not be negotiating after they arrive.
Footnotes
1. ASTM's official scope and procedures for Rockwell hardness testing of metallic materials. ↩︎
2. Detailed explanation of EDM's recast/white layer and microcracking risks for moldmakers. ↩︎
3. Official ASTM E384 standard scope for Knoop and Vickers microindentation hardness testing. ↩︎
4. ASTM's official scope for Brinell hardness testing of metallic materials. ↩︎
5. Detailed guide to D2 tool steel hardness ranges and tempering effects. ↩︎
6. Comprehensive H13 tool steel hardness data across heat treatment conditions. ↩︎
7. ASQ overview of the Z1.4 attribute sampling standard used for AQL inspection. ↩︎
8. Explanation of CNAS, China's national lab accreditation body for calibration traceability. ↩︎
9. Guide to hiring third-party inspectors like SGS and Bureau Veritas for steel parts QC. ↩︎
10. Recent study on recast layer thickness and microcracking from EDM thermal cycling. ↩︎



