 Skip to main content Skip to footer

Our shop once approved a Swiss-turned lot based on a thin FAI report. A missed thread callout led to a full line stoppage at the customer's plant.
A complete FAI report for Swiss CNC parts must include a fully ballooned drawing, full dimensional data for every characteristic, material and process traceability records, hardness and surface finish results, signed accountability forms, and a retained golden sample for future comparison.
Let's break down what belongs in each part of that report.
How many dimensions should be measured and reported in an FAI for a typical Swiss-turned part?
When our inspectors balloon a Swiss-turned drawing, we count every dimension and note, not just the critical ones. Skipping features always comes back to bite you.
An FAI for a typical Swiss-turned part should measure and report every dimension, GD&T callout, surface finish symbol, and drawing note on the print, not a sample. Most Swiss parts carry 40 to 80 ballooned characteristics, depending on complexity and feature count.
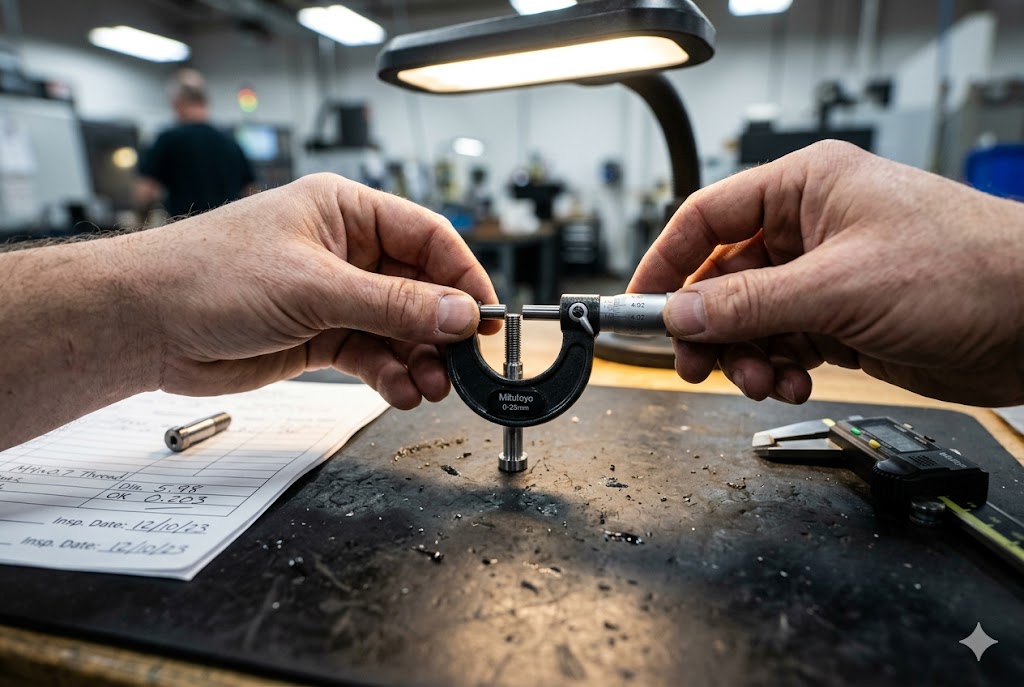
Counting dimensions sounds simple. In practice, it is the step suppliers shortcut the most. A real FAI is not a spot check on a few critical features. It is a full record of the part, line by line.
Why Every Feature Needs a Number
Each dimension, GD&T symbol 1, surface finish callout, and general note gets its own balloon number. This covers diameters, lengths, angles, chamfers, and thread callouts. Even a simple note like break all edges gets logged if it carries a tolerance. Nothing on the print gets skipped because it looks minor.
This full count matters because a feature left off the FAI is often the first feature to drift in production. We have seen suppliers balloon only the tightest ten dimensions and ignore basic step lengths. Those step lengths are usually the first to move once a tool wears down.
How Many Balloons Is Normal
A simple Swiss-turned pin with two diameters and one length might only need 10 to 15 balloons. A part with multiple diameters, a back-taper, a thread, and several GD&T calls can reach 60 or more. There is no fixed number. The drawing sets the count, not a template.
Threads Need Real Numbers, Not Just Go/No-Go
Thread data deserves special attention. A supplier who only reports go gauge pass and no-go gauge pass is not giving you the full picture. You also need an actual pitch diameter reading 2 from a thread micrometer or a CMM thread scan. This actual value tells you how close the thread sits to its limit, long before it fails a gauge check.
Matching Feature Type to Measurement Tool
Different feature types need different tools. Mixing this up leads to false confidence in the numbers.
| Feature Type | Typical Tool Used | Common Tolerance Range |
|---|---|---|
| Outer diameter | Micrometer or CMM | ±0.005 mm to ±0.02 mm |
| Position or concentricity | CMM 3 | 0.01 mm to 0.05 mm |
| Thread pitch diameter | Thread gauge plus micrometer or CMM | Class 4h/6H or tighter |
| Surface finish | Profilometer | Ra 0.4 µm to Ra 1.6 µm |
| Length or step feature | Height gauge or CMM | ±0.01 mm to ±0.05 mm |
Every row needs a real measured value on the report, plus the gage ID and its calibration due date. A pass mark alone is not proof. The number next to it is.
Should the FAI report include material certificate data, surface finish, and functional test results?
Our team has chased down mill certs after a supplier shipped a part with the wrong heat lot attached. A loose paper trail always shows up at the worst time.
Yes. A full FAI report must include material certificate data with heat or lot traceability, instrument-measured surface finish results against the drawing callout, hardness test data when specified, and any special process certifications for heat treat, plating, or passivation, each tied to a traceable lot.
Material data, surface finish, and function tests answer three different questions. Material data proves what the part is made from. Surface finish proves how it was finished. Function tests prove it actually works the way the design intends. A complete FAI answers all three, not just one.
Material Traceability Is More Than a PDF
A mill certificate alone is not traceability. The cert needs a heat or lot number that you can trace back to the actual bar stock used to machine the part. Add the material supplier's certificate of conformance and the manufacturer's own chemistry and mechanical test summary. Together these three documents form a chain you can follow, piece by piece, back to the melt.
Surface Finish Needs a Number, Not a Feel
A supplier who tells you a surface feels smooth has told you nothing useful. Surface finish on Swiss-turned bearing and sealing surfaces often calls for Ra below 1.6 µm 4. At that level, a finger test or a visual check cannot tell you anything reliable. You need an actual profilometer trace, recorded for each finish zone on the print, compared directly against the drawing callout.
When Hardness and Special Processes Apply
If the drawing calls out a hardness range or references a heat treat spec, the FAI needs a hardness test result. This should come from the actual FAI part or a witness coupon from the same heat, tested after machining, not pulled from the raw stock cert. Any secondary process, like passivation or plating 5, needs its own certification in the order it was performed.
| Documentation Type | What It Confirms | Common Reference Standard |
|---|---|---|
| Mill certificate | Raw material chemistry and heat lot | EN 10204 Type 3.1 6 |
| Surface finish report | Actual Ra/Rz vs. drawing callout | Profilometer trace per zone |
| Hardness test report | Heat treat result on actual part | Rockwell or Vickers, load noted |
| Special process cert | Passivation, plating, or anodize trace | AMS 2700, AMS 2759 |
Skip any one of these checks and you have a gap in the story. Gaps are exactly where disputes start later.
How do I use an FAI report to formally approve a supplier before releasing mass production?
We treat FAI sign-off as a gate, not a formality. Our team will not release a bar feeder run to volume until every form on the package is signed.
To formally approve a supplier, review the signed FAI accountability forms, confirm part number and drawing revision match the purchase order, verify the fixture and collet settings match production conditions, and retain a sealed golden sample before authorizing the supplier to run mass production.
Approving a supplier off an FAI is a process, not a single glance at a stack of paper. You are checking three things at once: the part itself, the paperwork behind it, and the setup that made it.
Check the Part Number Accountability First
Start with the basic accountability record. This should show the part number, drawing revision, purchase order reference, FAI report number 7, and the work order or router number used to make the part. Both the inspector who measured the part and a responsible quality engineer should sign and date the form. A report missing a signature or a date is not a finished report. It is a draft.
Confirm the Setup Was Stable, Not Hand-Dialed
For Swiss-turned parts, this step gets skipped more than any other. Ask for records showing the guide bushing clearance 8, collet bore size, and bar pusher setting used when the FAI part was made. These settings prove the part came from a repeatable production setup, not from a single hand-adjusted piece that nobody can reproduce at volume. Without this record, you have approved a part that the supplier may never make the same way again.
Hold a Golden Sample Before You Release Volume
Once the paperwork checks out, ask for a sealed or bagged sample tied to the FAI by a serial or lot number. Keep it on your side, not the supplier's. If a dispute comes up during production, this sample gives you something physical to compare against. It also gives you a reference point if the supplier changes bar stock or tooling later in the run.
| Approval Step | Who Should Sign or Hold It | Why It Matters |
|---|---|---|
| Part accountability form | Inspector and quality engineer | Confirms part, PO, and drawing rev all match |
| Setup and fixture record | Supplier production team | Proves the run is repeatable, not hand-fit |
| Characteristic data package | Inspector | Confirms every dimension was actually measured |
| Golden sample | Customer (you) | Gives a physical reference for future disputes |
Only after all four checks are closed out should you give the green light for mass production.
What happens if the FAI reveals that a critical dimension is out of tolerance?
We once held a full shipment after a single bore diameter failed FAI review. Letting that part through would have cost far more downstream.
When a critical dimension fails FAI, production should stop. The supplier must run a root cause analysis, correct the tooling or process, and submit a new FAI for that characteristic before mass production starts. Skipping this step risks the same failure repeating across the full run.
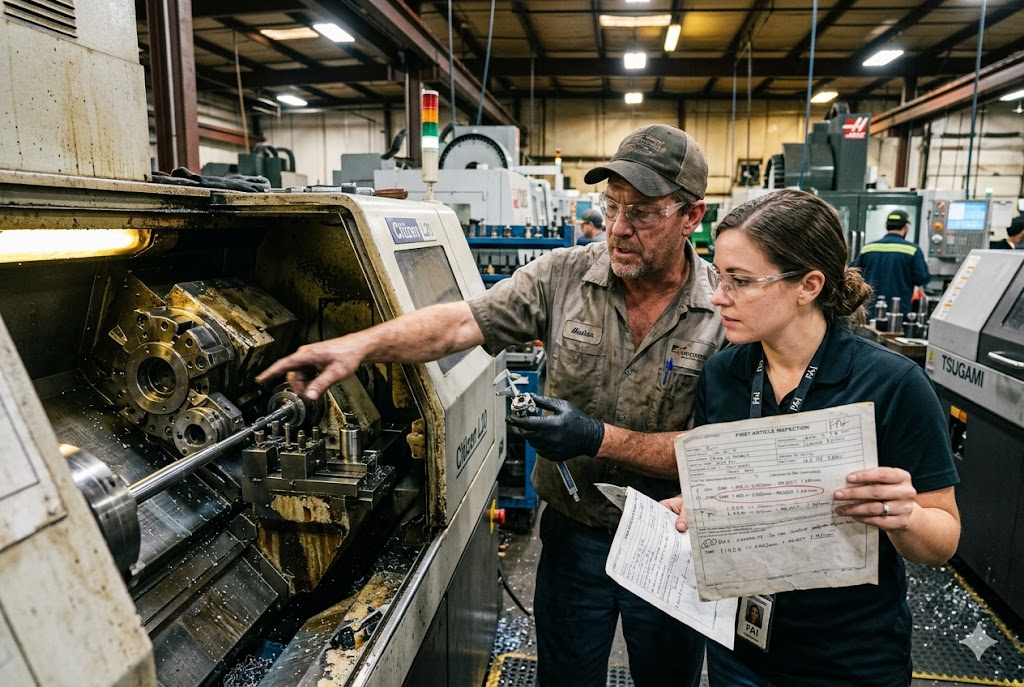
An out-of-tolerance result on a critical dimension is not a paperwork problem. It is a stop sign. The right response depends on how far off the part is and how it failed.
First, Separate Critical From Minor
Not every failure carries the same weight. A critical dimension usually controls fit, function, or safety, like a bore diameter that mates with another part, or a thread that carries load. A minor failure on a cosmetic edge break does not carry the same risk. Sort the failure type before deciding the next step.
Find the Root Cause Before You Touch the Tooling
Guessing at a fix wastes time and often creates a second problem. Common root causes on Swiss-turned parts 9 include tool wear, a worn guide bushing, bar stock that is slightly off in diameter, or a program offset that drifted. The supplier should trace the failure back to one of these causes, not just adjust the machine and hope it holds.
Decide the Disposition
Once the cause is known, someone has to decide what happens to the failed part and the rest of the lot.
| Failure Scenario | Disposition Option | Typical Next Step |
|---|---|---|
| Minor dimension drift, function unaffected | Use as is, with deviation approval | Customer sign-off on a documented concession |
| Critical dimension out of spec | Reject and rework or scrap | Correct tooling, remachine, re-inspect |
| Pattern across multiple parts | Containment plus corrective action 10 | Stop shipment, supplier corrective action report |
| Tooling or bar stock change identified | Process adjustment | Re-run FAI before resuming production |
Re-Run the FAI, Not Just the Part
After a fix, the supplier should submit a new FAI covering the affected characteristic, not just one good sample pulled by hand. A single good part after a fix does not prove the process is stable. A fresh FAI does.
Conclusion
A strong FAI report protects both sides before mass production starts. Get the full data, the signed forms, and a golden sample, and you avoid costly surprises later.
Footnotes
1. Explains GD&T symbols used on engineering drawings for manufacturing and inspection. ↩︎
2. Overview of thread inspection methods including pitch diameter measurement techniques. ↩︎
3. Primer on CMM technology and its role in precision dimensional inspection. ↩︎
4. Guide to surface roughness standards and Ra measurement using profilometers. ↩︎
5. Introduction to AMS 2700 passivation requirements for corrosion-resistant steel parts. ↩︎
6. Explains EN 10204 Type 3.1 mill certificates and material traceability requirements. ↩︎
7. Complete guide to AS9102 First Article Inspection Report forms and requirements. ↩︎
8. Overview of Swiss CNC turning, including guide bushing and collet setup details. ↩︎
9. Explains AS9102 FAI standard and its role in aerospace and precision part verification. ↩︎
10. Explains the supplier corrective action (SCAR) process and root cause analysis steps. ↩︎



