 Skip to main content Skip to footer

We have seen too many shipments arrive with missing or vague material documentation. When a part fails in the field and there is no MTR on file, the investigation becomes a costly guessing game for everyone involved.
To require your supplier to provide a Mill Test Report, specify MTR as a mandatory deliverable in your purchase order and quality clauses. State clearly that shipment acceptance depends on receiving a conforming MTR before or at the time of delivery. Define the required standard, grade, and heat number in writing.
Here is how to build a system that makes MTR compliance automatic — not an afterthought you chase down after the parts have already shipped.
What Information Must a Valid Mill Test Report Include for My QC Records?
Many purchasing teams accept whatever document a supplier sends and call it an MTR. Our quality team reviews hundreds of these documents each year, and a large share of them are missing fields that matter for real traceability.
A valid Mill Test Report must include the material grade, heat or cast number, chemical composition, mechanical test results, the producing mill's name, and the applicable standard. Without all of these fields, the document cannot support traceability or compliance verification.
The Core Fields Every MTR Must Contain
An MTR is only useful if it can answer one question: does this specific batch of material meet the specification I ordered? To answer that question, the document needs specific data — not general descriptions.
Here are the fields your QC record must capture from every MTR:
| Field | What It Must Show | Why It Matters |
|---|---|---|
| Material Grade | e.g., AISI 4140, SS316, 6061-T6 | Confirms the correct alloy was used |
| Heat / Cast Number | Unique identifier from the producing mill | Links document to physical material |
| Chemical Composition | Element percentages (C, Mn, Si, Cr, etc.) | Verifiable against the specified standard |
| Mechanical Properties | Tensile strength, yield strength, elongation, hardness | Confirms the material performs as required |
| Producing Mill Name | The actual steel or aluminum mill | Identifies the origin, not just the trader |
| Applicable Standard | ASTM, EN, JIS, or equivalent | Sets the pass/fail benchmark |
| Test Date | Date of material testing | Supports lot-based traceability |
| Certifying Signature | Authorized signatory at the mill or inspector | Establishes accountability |
EN 10204 Certification Types: Know the Difference
Not all MTRs carry the same weight. The European standard EN 10204 1 defines four types of inspection documents. For most industrial mechanical parts, you will encounter 2.2, 3.1, and 3.2.
| EN 10204 Type | Who Certifies | Independent Review? | Typical Use Case |
|---|---|---|---|
| 2.2 | Manufacturer (non-specific) | No | Low-risk, standard stock material |
| 3.1 | Manufacturer's own inspector | No | General commercial mechanical parts |
| 3.2 | Manufacturer + independent third party | Yes | Safety-critical, pressure, aerospace |
For most custom mechanical parts going into structural or load-bearing applications, EN 10204 3.1 is the minimum acceptable level. For safety-critical grades, require 3.2 and name the approved inspection body in your purchase order.
What to Do When Fields Are Missing
If a supplier sends an MTR with missing fields, do not accept the shipment. Send a written rejection notice citing the specific missing fields and the clause number in your quality agreement. Give a defined response deadline — typically five business days — and tie payment release to receipt of the corrected document.
This protects you legally and signals to the supplier that your documentation requirements are real, not negotiable.
Can a Chinese Supplier Provide a Mill Cert That Meets ASTM A29 or Equivalent Standards?
When our team sources raw material from Chinese mills for export orders, we often field this exact question from our US clients. The short answer surprises many buyers.
Yes, a Chinese supplier can provide a mill certificate that meets ASTM A29 or equivalent standards. Chinese steel mills such as Baosteel, HBIS, and Shougang produce material tested and certified to ASTM, EN, and JIS standards. The key is specifying the standard explicitly in your purchase order and verifying the mill of origin.
How Chinese Mills Certify to ASTM Standards
ASTM A29 2 covers general requirements for steel bars in the hot-wrought condition. It is widely used for shafting, gears, and structural mechanical components. Major Chinese mills routinely test and certify to ASTM because their largest export markets — the US and Europe — require it.
The problem is not usually the mill. The problem is the supply chain between the mill and your supplier.
In China, a fabricator or machining shop rarely buys material directly from the mill. They buy from a trading company or service center. By the time material reaches your supplier, it may have passed through two or three hands. At each step, documentation can be lost, substituted, or altered.
The Sub-Tier Problem: Where Grade Swaps Happen
| Supply Chain Level | Risk Level | Common Issue |
|---|---|---|
| Producing Mill | Low | Mill-certified material, full documentation |
| Steel Trading Company | Medium | Mixed lots, documentation gaps |
| Material Service Center | Medium-High | Possible substitution without disclosure |
| Fabricator / Machining Supplier | High | May use lower-grade stock to reduce cost |
To manage this risk, name the approved mill explicitly in your purchase order. State that only material sourced from the named mill is acceptable. Require the MTR to show the producing mill's name — not just the trading company's stamp.
Domestic Chinese Standards vs. ASTM Equivalents
Chinese suppliers sometimes offer GB (Guobiao) standard certificates instead of ASTM. In many cases, there are close equivalents, but the chemical composition windows and testing requirements are not always identical.
If your design specifies ASTM A29 Grade 4140, accept only an ASTM-certified MTR. Do not accept a GB/T 3077 certificate as a substitute unless your engineering team has reviewed and approved the equivalence in writing. Never let the supplier make that equivalence determination on your behalf.
Requesting a Dual-Standard Certificate
Some major Chinese steel mills 3 can issue dual-standard certificates — for example, certifying to both GB/T and ASTM in one document. This is useful when the part will be manufactured in China but must meet US specifications. Ask your supplier to confirm whether the mill can issue this format before you place the order.
How Do I Verify That the MTR Provided Matches the Actual Material Used in My Order?
This is the question most buyers forget to ask. Receiving an MTR is easy. Confirming that the MTR actually matches the physical material in the box is a completely different task.
To verify that an MTR matches the actual material, cross-reference the heat number on the document against the physical markings on the material itself, and use XRF spot-checks on received stock to independently confirm the chemical composition declared on the certificate.
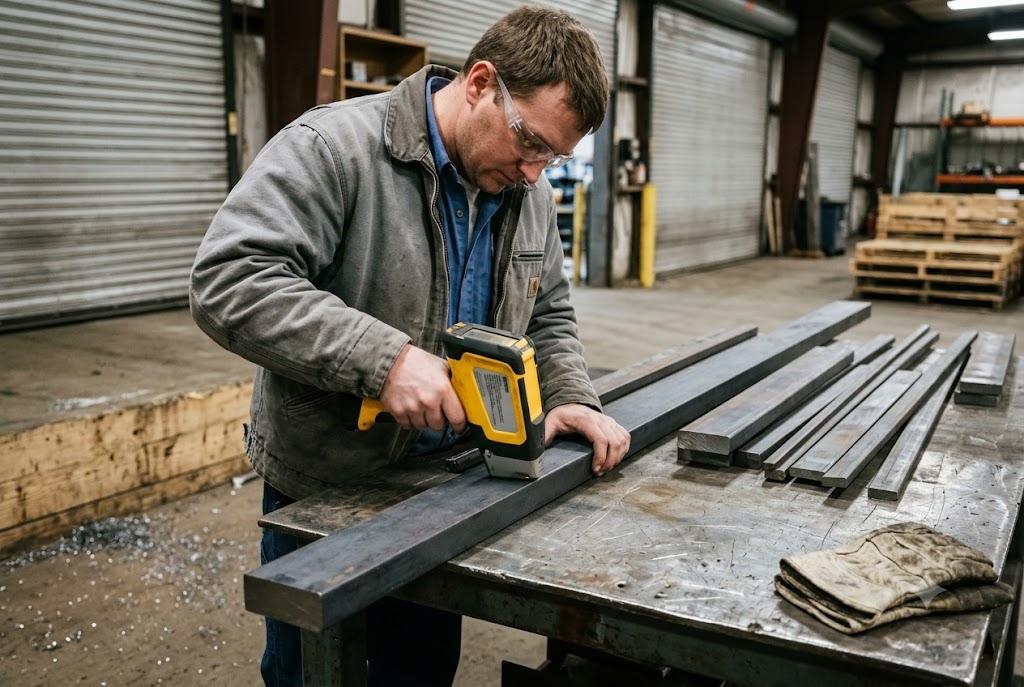
Step One: Physical Heat Number Matching
Every batch of mill-certified material should carry a physical mark — stamped, stenciled, or tagged — with the heat or cast number 4. When the material arrives, your receiving team should compare this number to the heat number on the MTR. They must match exactly.
If the supplier cannot demonstrate a heat number match — because the marks have been removed, the tag is missing, or the numbers differ — do not accept the material. Treat it as an unverified lot until the supplier provides documentation that reconciles the discrepancy.
Step Two: XRF Spot-Check Verification
An XRF (X-ray fluorescence) analyzer 5 is a handheld device that reads the elemental composition of metal alloys in seconds. It is not a laboratory-grade test, but it is fast, non-destructive, and accurate enough to catch grade substitutions.
Define a sampling plan in your incoming inspection procedure. A common approach:
- Lots of 1–10 pieces: test 100% of pieces
- Lots of 11–50 pieces: test a minimum of 5 pieces
- Lots of 51+ pieces: test 10% of pieces, minimum 10
If any XRF reading falls outside the composition range declared on the MTR, quarantine the entire lot and initiate a supplier corrective action request 6.
Step Three: Cross-Reference Against Mill Production Records
For critical applications, your quality agreement should include a right-to-audit clause. This gives you the contractual right to request that the supplier cross-reference the heat number against the originating mill's internal production records. Some mills publish heat record lookups through their customer portals. For others, you must request the records through your supplier.
This step adds time but is essential for aerospace, medical, or pressure-rated components where material traceability 7 is a regulatory requirement — not just a quality preference.
Building a Traceable Filing System
Once MTRs are verified, they must be filed in a system that allows rapid retrieval. Index every MTR by:
- Heat number
- Purchase order number
- Part number
- Date received
If a field failure occurs six months later, you need to pull the MTR for the affected lot within minutes — not days. A spreadsheet-based log is acceptable for small volumes. For higher volumes, use a document management system with search by heat number.
Should I Request MTRs at the Purchase Order Stage or Only at Pre-Shipment Inspection?
Buyers who wait until pre-shipment inspection to request MTRs are already too late. By that point, the material has been cut, machined, and processed — and switching it out is no longer practical.
You should request MTRs at the purchase order stage. Specify MTR as a required deliverable in your PO quality clauses, with review and acceptance required before production begins. Tie final payment or a retention percentage to verified MTR receipt, creating financial leverage for early compliance.
Why the PO Stage Is the Only Logical Point
When a supplier purchases raw material, the MTR is generated at that point by the mill. If you do not specify requirements before material is procured, the supplier will buy whatever is available at the best price. After the fact, they cannot go back and get an MTR for a different standard or grade.
Requiring MTR submission before production begins gives you:
- Time to review the document before any machining starts
- The ability to reject non-conforming material before it becomes a finished part
- A clear record that the correct material was approved before work began
Payment Milestones as Compliance Levers
Structure your payment terms to create real financial incentives for MTR compliance. A typical structure that works well:
| Payment Milestone | Condition |
|---|---|
| 30% deposit | PO acceptance + MTR requirement confirmed in writing |
| 40% progress payment | MTR received, reviewed, and accepted by buyer's QC |
| 30% final payment | Pre-shipment inspection passed + MTR filed in buyer's system |
With this structure, no supplier can ship without an accepted MTR — because the money is not released until that step is complete.
What to Include in the PO Quality Clause
Your purchase order quality clause for MTR requirements should state:
- The specific standard and grade required (e.g., ASTM A29 Grade 4140)
- The EN 10204 certification type 8 required (3.1 or 3.2)
- The named mill of origin (if applicable)
- The deadline for MTR submission (e.g., within 5 business days of material receipt by supplier)
- The consequence of non-submission (shipment hold, payment retention)
- The MTR falsification clause: fraudulent or altered MTRs constitute material breach, triggering full cost recovery
Put these terms in writing in every PO. Do not rely on verbal agreements or email confirmations that are not tied to the order document itself.
Pre-Shipment Inspection: A Second Checkpoint, Not the First
Pre-shipment inspection is still valuable — but as a verification checkpoint, not a first request. By the time PSI occurs, your MTR should already be on file, reviewed, and approved. The PSI inspector's job is to confirm that the heat number on the physical material 9 matches the MTR already in your system. That is a two-minute check, not a three-day document chase.
Conclusion
Requiring an MTR is straightforward. Enforcing it takes a system. Build your requirements into the PO, tie payment to compliance, verify the physical material, and file everything by heat number. That chain is your protection. For further reading on how metal supply chain traceability 10 supports quality audits and compliance across the full procurement cycle, industry resources from certified material suppliers offer additional practical frameworks.
Footnotes
1. Explains the four EN 10204 certificate types and the key differences between 3.1 and 3.2. ↩︎
2. Official ASTM A29 standard page covering general requirements for hot-wrought carbon and alloy steel bars. ↩︎
3. Overview of leading Chinese steel mills that certify to ASTM, EN, and JIS international standards for export. ↩︎
4. Wikipedia definition of heat number and its role in linking physical material to mill test records. ↩︎
5. AZoM guide to handheld XRF analyzers for metal alloy identification and incoming inspection quality control. ↩︎
6. Propel Software glossary entry explaining the SCAR process for addressing supplier nonconformances formally. ↩︎
7. Xometry explainer on material traceability fundamentals, including heat number tracking and MTR filing. ↩︎
8. Detailed breakdown of EN 10204 certificate types 2.1, 2.2, 3.1, and 3.2 for industrial procurement. ↩︎
9. Industrial Metal Supply article on why material traceability and heat number tracking protect manufacturers. ↩︎
10. Fry Steel overview of material traceability as a supply chain differentiator, covering audits and compliance. ↩︎



